When Atlas Iron and Roy Hill formally joined forces to become Hancock Iron Ore, it marked the beginning of a new chapter for one of Australia’s leading iron ore businesses. The move brought together two companies with deep Pilbara experience, complementary strengths and a shared focus on safe, reliable and efficient mining.
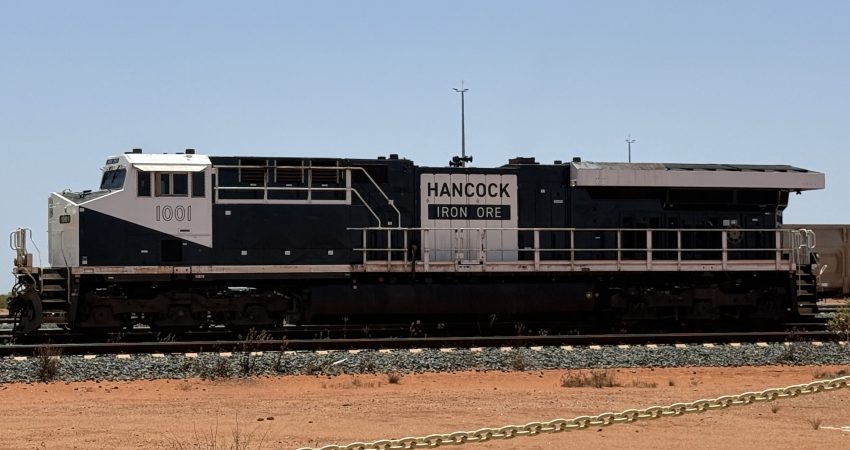
For Duratec, this transition created an opportunity to support a visible, large-scale fleet identity program across 28 locomotives and four class track motor vehicles, applying the new Hancock Iron Ore identity with precision, quality and respect for the legacy of both businesses.
A highly technical process
Rebranding rolling stock is far more complex than applying a new coat of paint. Each locomotive undergoes a carefully controlled process designed to ensure durability, quality and compliance with stringent safety and technical requirements.
The process begins with the removal of existing hard plastic decals, which are scraped back before the entire surface is pressure washed to eliminate contaminants.
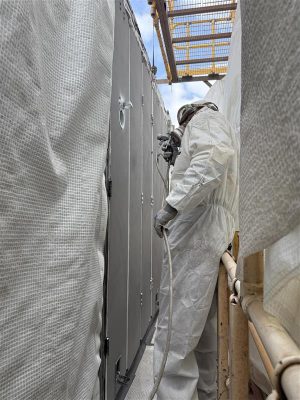
Applying the first coat of paint to the east and west side of the panel for locomotive 1014.
Encapsulation is then installed within the panels to prevent dust ingress into the engine bay, while end-capping protects adjacent areas during blasting.
Paint application is closely monitored through Dry Film Thickness (DFT) testing, with approximately 24 readings taken on each side of every locomotive. An initial coat is applied to achieve a thickness of 150 microns, followed by additional coats that bring the final specification to 200 microns.
From preparation to final coating, each locomotive requires three to four days to complete, allowing for multiple coatings, inspections and drying times.
Managing conditions and expectations
Working in the Pilbara presented its own challenges. Humidity levels must remain below 85 per cent before coating activities can proceed, making environmental conditions a critical factor in project delivery.
Between December and March, elevated humidity regularly delayed start times, requiring the team to remain flexible and strategically adjust work schedules to maintain quality standards while meeting program requirements.
Expertise behind the transformation
For Duratec Superintendent North-West, Steven Holland, the project ranks among the most technically demanding of his career.
Having started his career with Duratec as a carpenter before transitioning into Blast and Paint, Steven has led work on major projects including BHP’s first C&D refurbishment and numerous maintenance programs for Fortescue.
With the importance of this rebrand for a major mining company, the quality had to be spot on. Bringing in automotive painters allowed us to achieve the level of detail and finish the project deserved.” – Steven Holland, Superintendent North-West
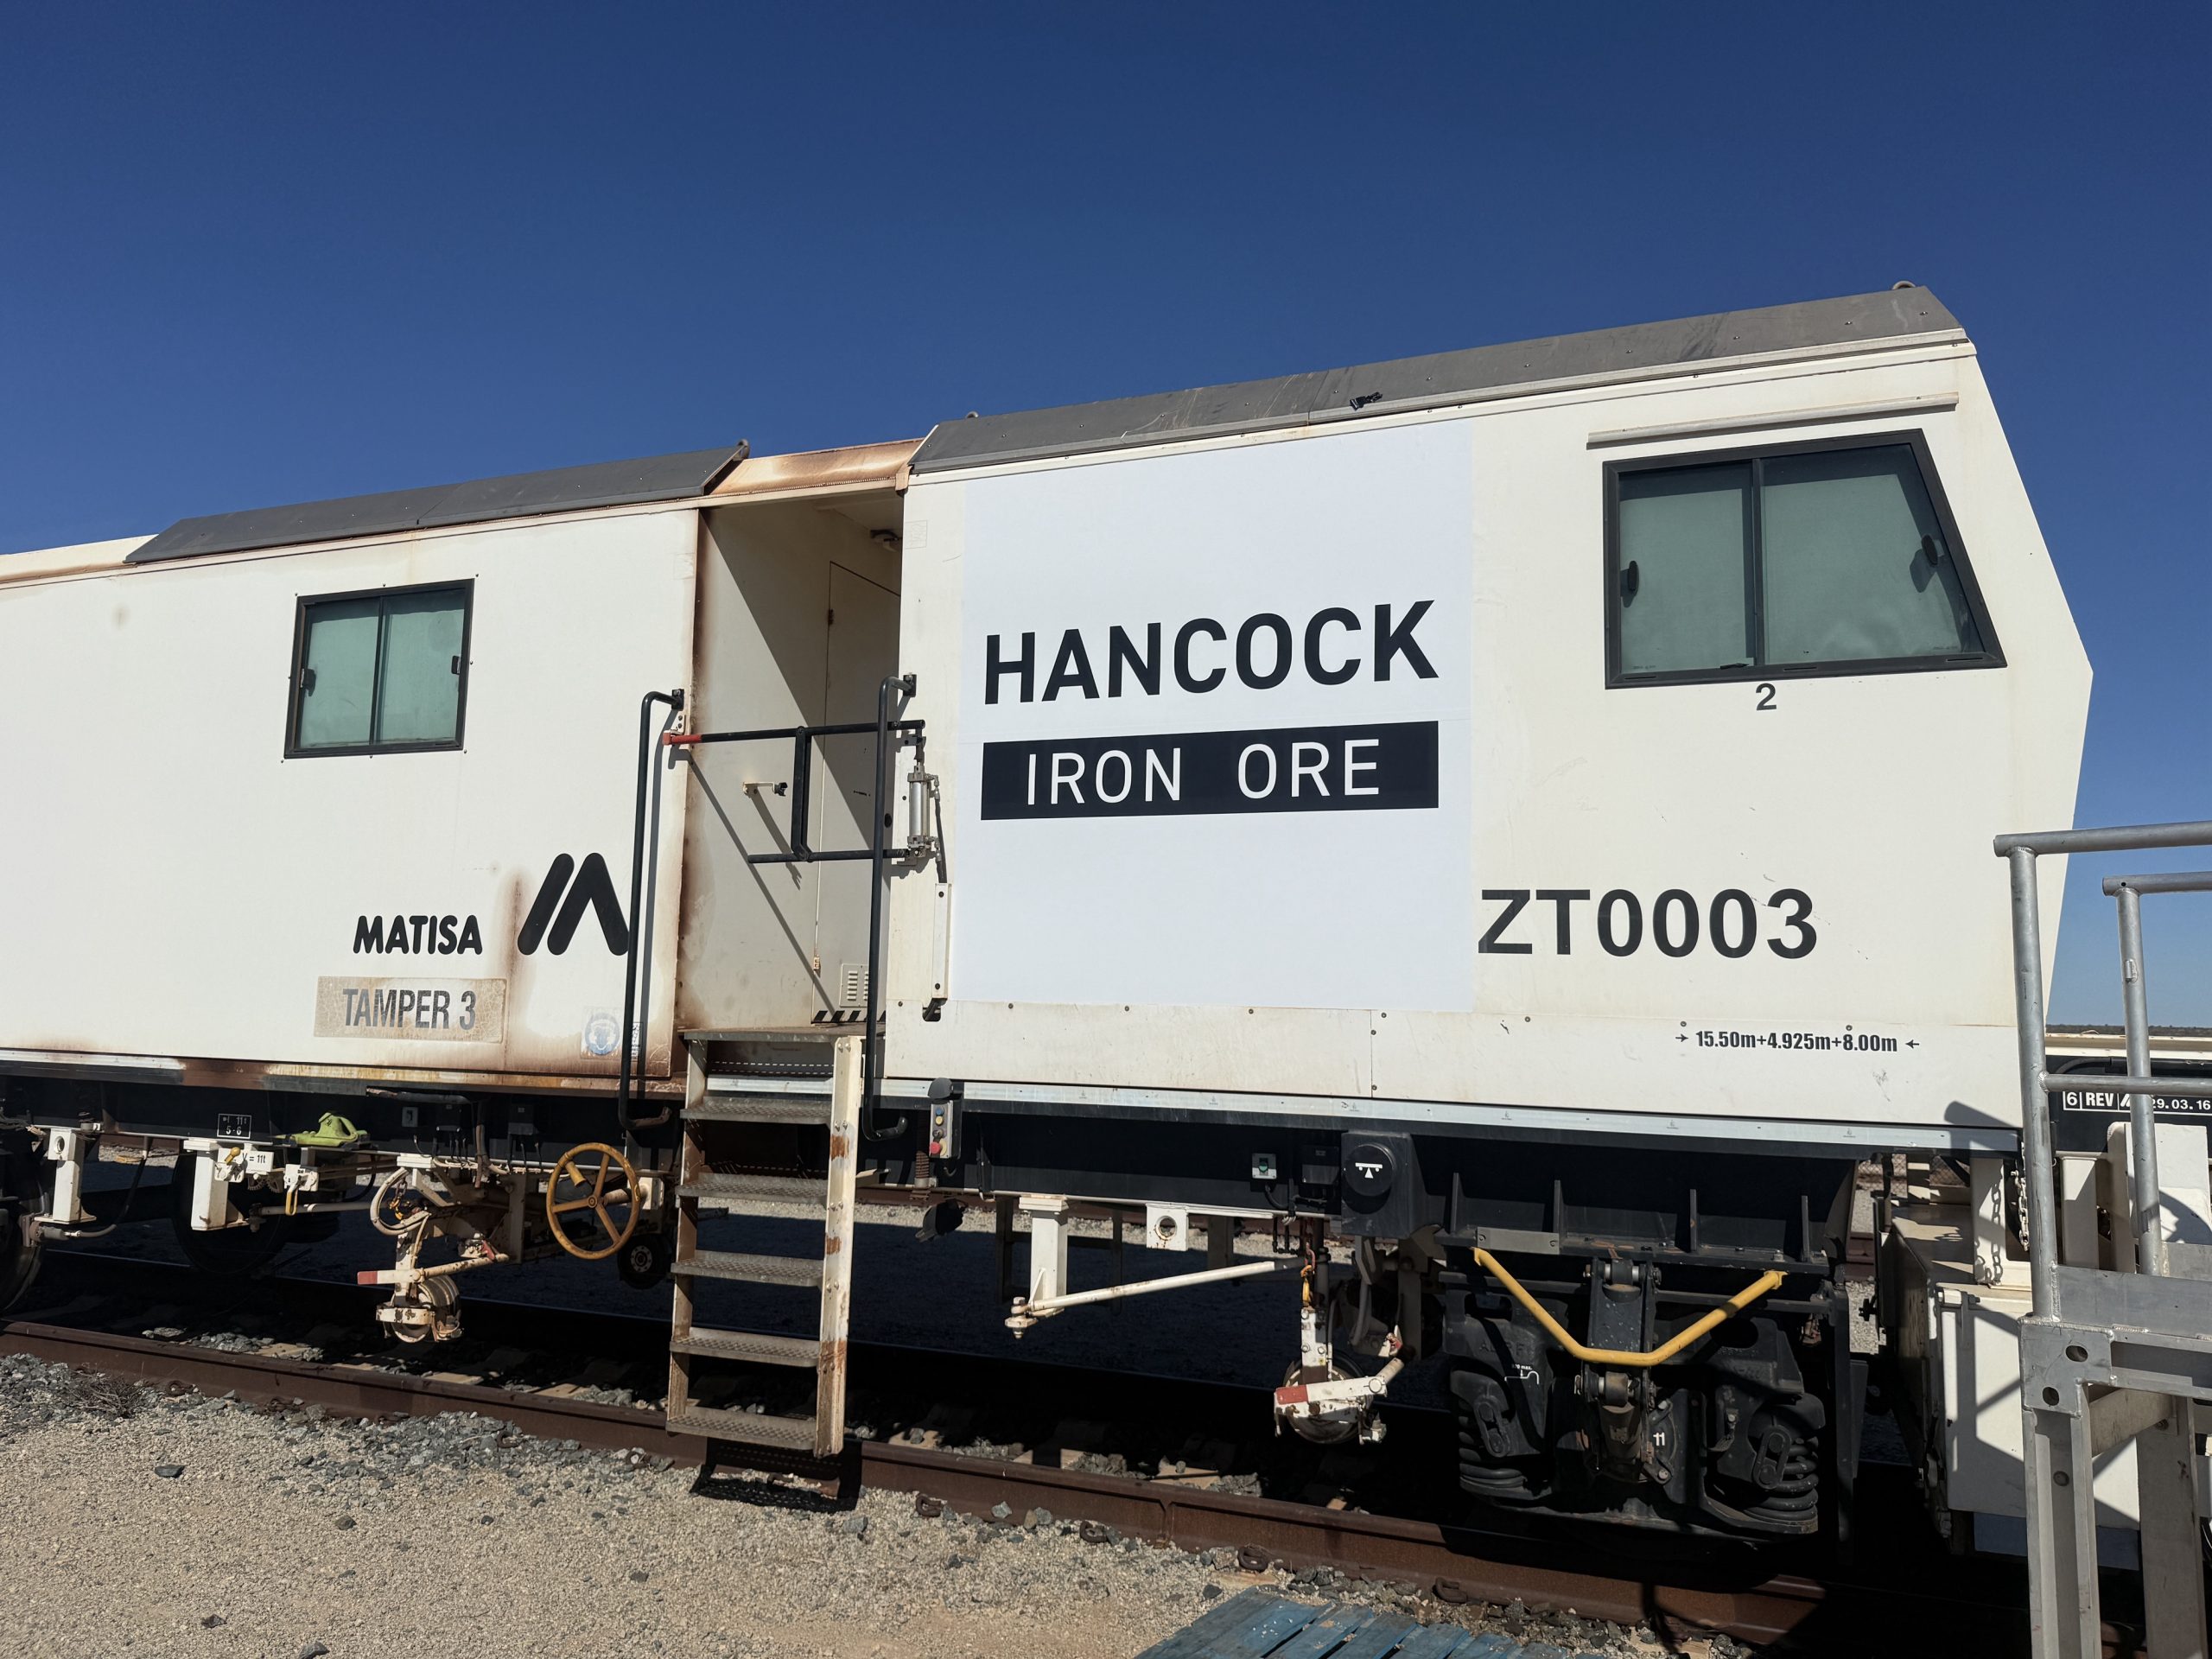
Final product of Tamper 3 – one of Hancock Iron Ore’s rail machines.
Today, the completed fleet carries more than a new name. It reflects Duratec’s commitment to quality, technical excellence and collaborative project delivery, demonstrating the team’s ability to execute complex rebranding programs safely and successfully at scale.